How modern tire retreading cuts cost per mile for small fleets
Automated buffing, laser-guided tread application, and precision curing have turned a labor-intensive craft into a manufacturing process that delivers 500,000-mile casings at half the cost of new rubber.
How much does a retread save per tire compared to new rubber?
A retread costs roughly half what a new replacement tire costs, and fleets with effective retread programs routinely get over 500,000 miles out of every new tire and its subsequent retreads. The U.S. market splits evenly between new replacement tires and retreads, about 15 million units each per year, which tells you the economics work for the fleets running the highest annual mileage.
The process has changed. What used to require a technician with a strong back and a steady hand to manually guide a 50-pound roll of tread rubber onto a spinning casing is now handled by automated builders that measure diameter with lasers, cut the tread to exact length, and center it so the pattern matches perfectly at the splice. The result is a more uniform product with fewer variables introduced by human error.
What changed in the buffing and inspection process
Before any tread goes on, the casing gets inspected and buffed to remove the old tread down to a precise radius and diameter. Older retread plants relied on a technician's eye and hand to hold the buffer steady. Modern plants use computerized buffers that hold the exact radius across the entire circumference. Casing defects get flagged before the tire reaches the buffer, so damaged units don't waste time in the build queue.
When rocks or road debris have damaged the casing down to the steel belts without puncturing the innerliner, a technician removes the damaged rubber in what's called a skive and fills it with raw rubber from an extruder gun. Modern cushion gum extruders fill these small repairs while maintaining a perfectly even layer of uncured rubber across the entire casing, which eliminates the need for cement and creates a more uniform bonding surface.
Mold cure vs. precure: two systems, same automation trend
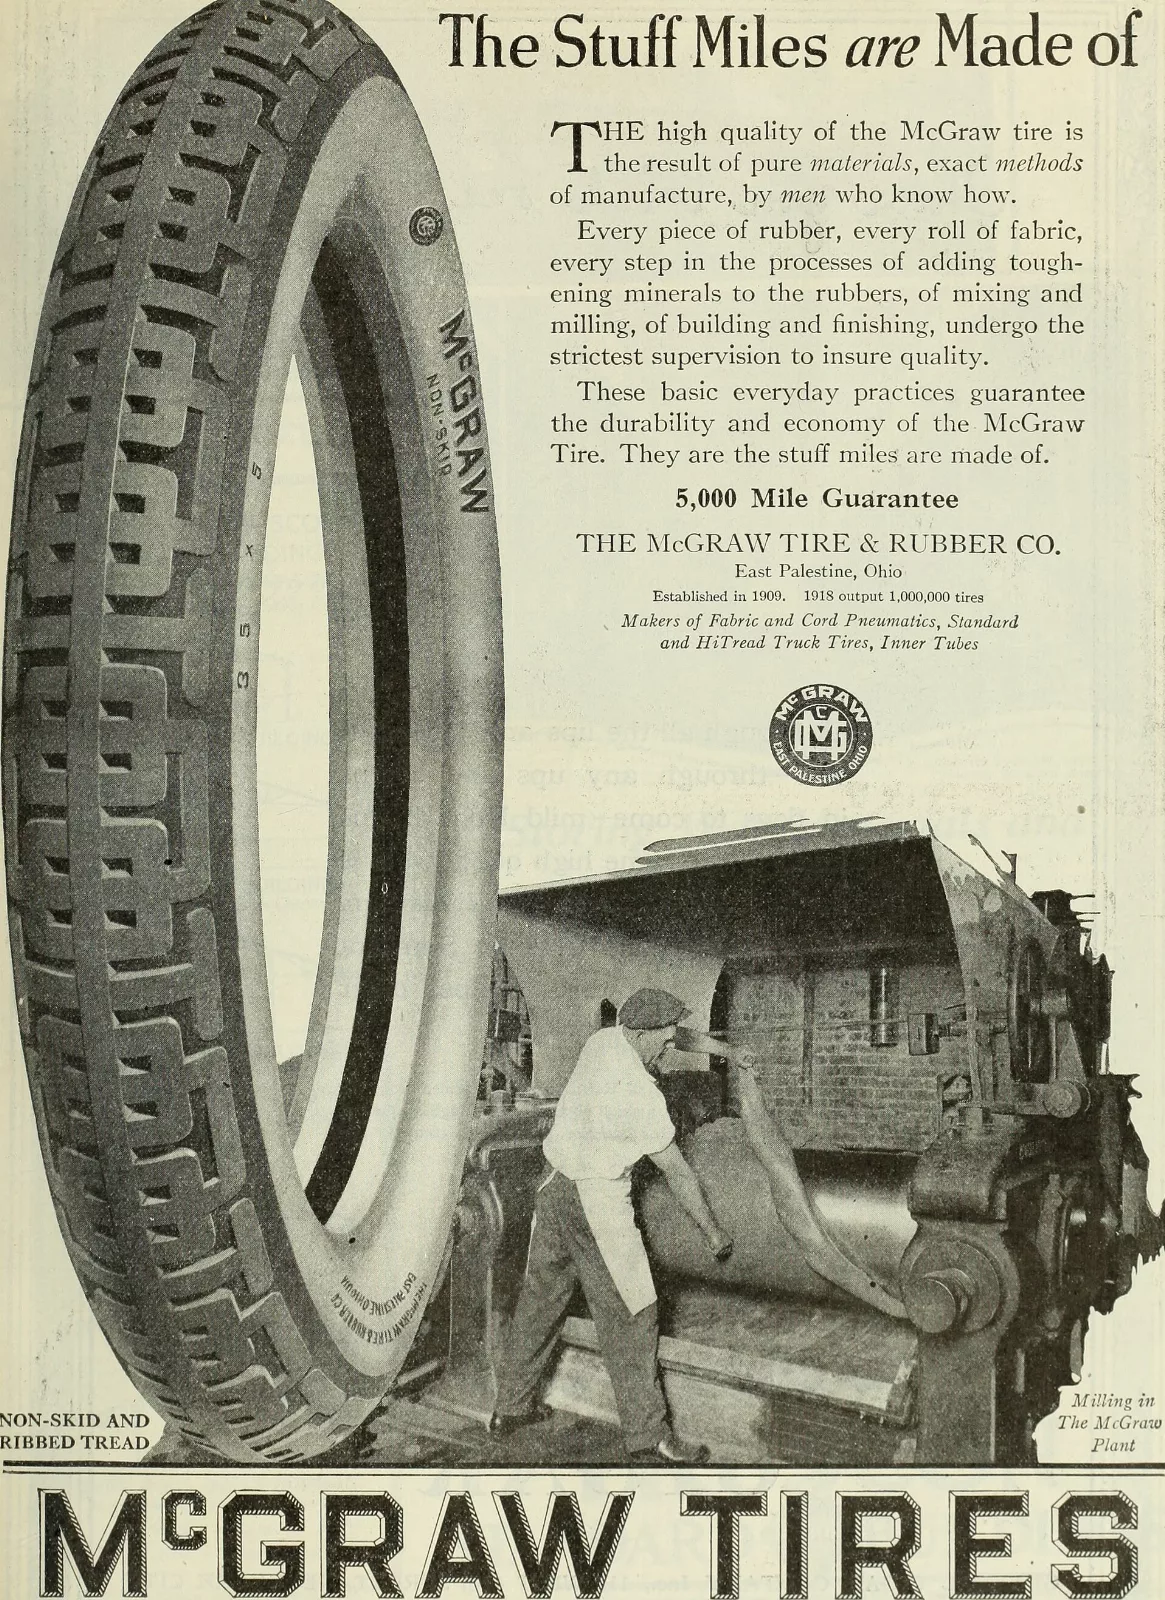
Retread plants use two tread application methods. In mold cure, technicians apply raw rubber to the buffed casing as one continuous thin strip, building it up in layers until it reaches the proper radius and diameter. The process mirrors new tire manufacturing. Older plants depended on a technician to guide the strip by hand. Modern mold cure plants use automated builders that apply the rubber to the millimeter.
In precure retreading, the tread rubber arrives already cured in rolls. Technicians used to unroll it onto the casing as it rotated, a process that required strength and skill to keep the tread centered and straight. The tread pattern rarely matched at the splice because the technician had to eyeball the cut length. Today's precure plants use automated builders that measure the casing diameter, lay out the tread on a roller table, cut it to exact length so the pattern matches at the splice, and use lasers to guide it onto the casing perfectly centered. From the technician's perspective, it requires far less effort and skill than the previous generation of equipment.
Both systems require a thin layer of uncured rubber called cushion gum to bond the tread to the casing. Cushion gum used to come in rolls that technicians cemented onto the casing by hand. Modern extruders apply it in a perfectly thin and even layer, improving efficiency and accuracy.
How curing locks the tread to the casing
Mold cure retreads go into a mold that closes around the tire and imprints the tread design under heat and pressure, the same process used for new tires. The casing and raw rubber must be exact in diameter. Too much rubber and the casing buckles under pressure. Too little and the mold won't fill completely, leaving areas where the tread isn't fully imprinted. The process requires precision in buffing and building before the tread can be cured.
Precure retreads get placed in a rubber envelope that seals at the beads. A vacuum pulled through a special valve creates pressure on the tread, pressing it onto the casing. Some plants add a second envelope inside the tire to create internal pressure that sandwiches the tread between the two envelopes. The tire then goes into an autoclave, a pressure chamber that preserves the vacuum on each tire while adding heat and pressure to fully cure the tread rubber to the casing. After a few hours, the bond is complete.
What the environmental and safety data show
Retreading saves enough energy to power over 1.1 million homes for a year, saves 343 million gallons of oil, and diverts 663 million pounds of landfill material, reducing tire waste by 473 million pounds, according to the Tire Retread and Information Bureau. The fact that new replacement tires and retreads split the market evenly, about 15 million units each per year, supports the lower operating cost claim.
Tire debris on the roadside splits equally between new tires and retreads. Most roadside debris shows exposed steel belts, which means the casing failed. When a retread fails, the belts remain intact because the tread separates from the casing. Casing failure is almost always caused by underinflation or overloading. The resulting internal heat buildup will cause a new tire to fail the same way. Retreads have a safety record equal to new tires when properly inflated and maintained.
What this means for small fleets and owner-operators
Without retreads, trash haulers and recycling fleets (both heavy retread users) would see operating costs jump, and those costs would pass through to everyone else. Reliance on oil for new tire production would increase, pushing energy costs higher. For a small fleet running regional or line-haul, an effective retread program is the difference between achieving the lowest cost per mile and burning capital on new rubber every 150,000 miles. The Michelin X Multi Energy D2 regional tire targets a 1-million-mile casing with reinforced sidewalls, which means more retread cycles per original casing if the fleet manages inflation and load discipline.
Automation has made the retread more reliable than it was a generation ago. Computerized buffing, extruded cushion gum, laser-guided tread application, and precision curing reduce the variables that used to depend on a technician's skill. The product is more uniform. The economics still favor the fleet that can preserve casing assets across multiple retread cycles.